
CATERPILLAR E365 / E374 Excavator Drive Sprocket Wheel Assembly / Sprocket Wheel Group (P/N: 141-9655) – Travel Drive Components for Caterpillar Heavy-Duty Crawler Excavators and Rotary Blast Hole Drills. Manufactured by CQC Track


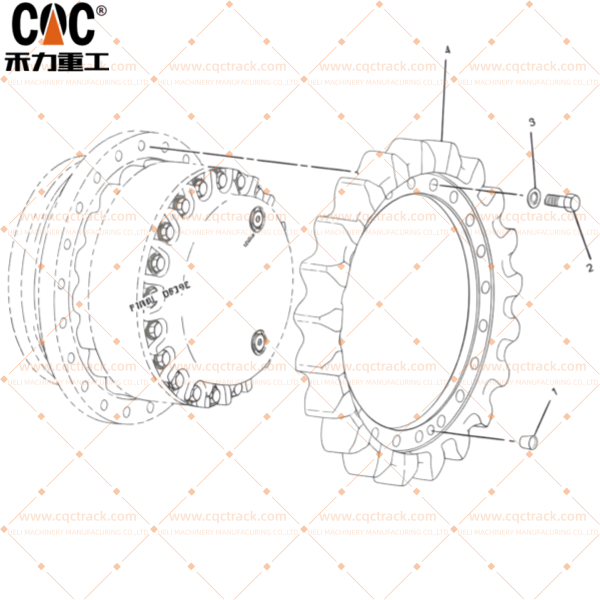
On a 65-tonne to 75-tonne class crawler excavator such as the CATERPILLAR E365 or E374, the final drive sprocket is the singular component that converts hydraulic motor torque into tractive effort. It meshes continuously with the heavy track chain, transmitting enormous drawbar pull while enduring abrasive rock dust, impact shock from tramming over broken ground, and the relentless cyclic loading of mining and mass excavation duty cycles. For the CATERPILLAR E365 and E374, including the 345C, 365B, 365C, 374D, and 374F excavator platforms, as well as compatible rotary blast hole drill applications, sprocket integrity is a direct determinant of track chain life, undercarriage alignment, and overall machine productivity . CQC Track, the specialized tracked chassis manufacturing division of CQC International, delivers a premium, OEM-caliber replacement Drive Sprocket Wheel Assembly / Sprocket Wheel Group, precisely interchangeable with CATERPILLAR genuine part number 141-9655 . This is not a generic aftermarket wheel — it is a precision-engineered final drive component built within the same active OEM production ecosystem that serves multiple global equipment leaders, and refined through two decades of continuous field feedback. Authored by Jack, with dedicated international support from Philip and Haily, this technical overview explains why CATERPILLAR E365 and E374 fleet operators trust CQC Track for travel drive components that match the durability of the original equipment.
1. Manufacturer Strength: Embedded OEM Production with Full In-House Capability
The performance and service life of a final drive sprocket are predetermined by the manufacturing environment in which it is produced. CQC Track operates a fully integrated, self-built industrial campus where every production line is company-owned and directly controlled. We do not outsource critical processes. Our factory currently operates as a certified OEM manufacturing base for the global heavy equipment industry, supplying complete track assemblies, rollers, idlers, and sprockets to Hitachi, Kobelco, LiuGong, XCMG, and SDLG, as well as serving as an OEM and ODM partner for Caterpillar-compatible undercarriage solutions . This embedded OEM reality means the CATERPILLAR E365 / E374 141-9655 Drive Sprocket Assembly is produced on the identical forging presses, heat-treatment furnaces, and CNC machining centers that serve Japanese, Korean, and Chinese OEM assembly lines. The material certifications, process controls, and quality gating applied to this sprocket are exactly those mandated by the world’s most rigorous equipment manufacturers. Furthermore, CQC Track is structured to offer comprehensive OEM customization and ODM manufacturing — whether adapting tooth profiles for specific applications, modifying mounting interfaces, or developing proprietary branded sprocket lines for distributors and fleet operators .
2. Technical Architecture: Forged, Heat-Treated, and Precision-Machined for Extreme Duty
A final drive sprocket on a 65-tonne class excavator must simultaneously resist tooth flank abrasive wear, root bending fatigue, and internal bearing contamination. The CQC Track 141-9655 Sprocket Wheel Assembly is constructed through a deliberately sequenced, high-integrity manufacturing process where every step is designed for repeatability and dimensional precision.
- Closed-Die Hot Forged Alloy Steel Sprocket Rim: The toothed drive rim originates as a solid billet of high-grade alloy round steel, which is heated to approximately 1150–1250°C until fully austenitized and then subjected to high-pressure deformation between precision-machined dies in multiple closed-die forging stages . This process eliminates the internal porosity, voids, and microstructural inconsistencies inherent in cast or fabricated alternatives, delivering a monolithic structure with exceptional resistance to bending fatigue, tooth root cracking, and impact-induced fracture. The forging process fundamentally enhances the component’s mechanical properties compared to cast alternatives, aligning the internal grain flow precisely with each tooth contour .
- Integral Quench and Temper Treatment: Prior to any finish machining, the entire forged sprocket body undergoes a rigorous through-quenching and tempering cycle . This foundational heat treatment uniformly refines the core microstructure into tempered martensite, providing an optimal combination of high tensile strength and ductile toughness that prevents permanent tooth deformation or brittle failure under extreme torque loads.
- Precision CNC Machining and Induction-Hardened Tooth Profiles (55–62 HRC): Following rough machining to near-net geometry and precision CNC finishing to exact OEM dimensional tolerances — including the critical 608 mm inner diameter specification for the 141-9655 — the tooth flanks and drive engagement surfaces are selectively hardened through a controlled medium-frequency induction hardening process. The surface hardness is consistently maintained between 55 and 62 HRC, creating a deep, wear-resistant case that dramatically reduces abrasive tooth wear, “hooking” deformation, and pitch-line spalling. Critically, the ductile, tempered core beneath the hard case absorbs dynamic shock without crack propagation, ensuring a sprocket that is both wear-resistant and impact-tolerant. The 141-9655 sprocket features 21 teeth and is designed for a secure, accurate fitment on the final drive output interface .
- Dual-Seal-Groove Shaft and Top-Tier Floating Seal System: The sprocket mounting interface is precision-ground with a dual seal groove profile, forming a labyrinth that accommodates a top-tier duo-cone floating seal set. This face-to-face metal sealing technology is the global benchmark for the absolute exclusion of water, mud, fine silica dust, and abrasive mining slurry from the internal bearing cavity. The fully sealed cavity is factory-filled with a specially formulated low-temperature-resistant anti-freeze grease, guaranteeing immediate full-film lubrication at every startup and continuous corrosion protection from Arctic deep-freeze to tropical monsoonal humidity.
- Spheroidal Graphite (Ductile) Iron Side Covers: The sealing side covers are manufactured through a precision spheroidal graphite iron casting process, deliberately selected for its exceptional dimensional stability, wear resistance, and ability to maintain a flawlessly smooth, hard mating surface that preserves uniform floating seal compression over the sprocket’s entire service life.
3. Twenty Years of Continuous Process Refinement, Validated in Global Extreme Mining
The CQC Track 141-9655 Sprocket Wheel Assembly is not a static design; it is the direct product of a 20-year continuous engineering improvement cycle, driven entirely by failure mode analysis and wear data harvested from the planet’s most demanding extraction and construction environments. Our sprockets have been systematically tested, analyzed, and incrementally refined through sustained operation in the deep-level gold and platinum mines of South Africa, the high-altitude copper and silver pits of Peru and Ecuador, the frozen iron ore basins of Russia, the abrasive hard-rock quarry and demolition sites of South Korea, the large-scale infrastructure and mining projects of India, and the tropical construction and extraction operations of Vietnam. Every design parameter — from optimizing the tempering curve to eliminate residual stress concentrations, to precisely calibrating the induction hardening scan speed for a flawless hardness gradient, to validating the long-term pumpability of the anti-freeze grease across extreme temperature swings — has been engineered directly back into our production standard. The quality stability and operational reliability of today’s sprocket assembly are not catalog promises; they are field-verified attributes proven over millions of machine operating hours on every continent.
4. A Complete, Matched Undercarriage Component Ecosystem
A final drive sprocket does not function in isolation. Installing a premium-grade sprocket alongside worn track chains, marginal lower rollers, or a fatigued idler creates a costly mismatch in component life that rapidly accelerates system-wide undercarriage deterioration. As a specialist manufacturer of complete tracked chassis solutions, CQC Track eliminates this risk by producing a comprehensive, in-house suite of related undercarriage parts for the CATERPILLAR E365, E374, and the broader 345/365/374 excavator series, as well as compatible rotary blast hole drill applications. Our production program includes matched track link assemblies with induction-hardened pins and bushings, track bottom roller assemblies(366-3380), front idler wheel assemblies(248-7256/136-2429), and upper carrier rollers(542-8380), all manufactured within a unified metallurgical and thermal processing envelope . This integrated approach ensures consistent wear rates and predictable life cycles across all undercarriage components. The CQC International business team — comprising Philip, Jack, and Haily — is structured to supply these components as synchronized, kit-based deliveries, ensuring your maintenance operation receives a fully harmonized set of parts designed to deliver consistent, engineered performance.
5. Global Export Reach into Quality-Conscious Mining and Construction Markets
CQC Track heavy-duty mining and construction undercarriage components are exported with full confidence into markets that enforce the most stringent import quality and performance standards. Our CATERPILLAR E365/E374 sprocket assemblies and complete undercarriage kits are actively supporting excavator and drill fleets across South America (Ecuador, Peru), Southern Africa, the Russian Federation, South Korea, and high-end application segments in India. Our international distribution network further extends to the South Pacific island nations, Vietnam, Kazakhstan and the broader Central Asian corridor, Turkey, and North America. This sustained and widespread global acceptance — spanning equatorial heat, arid desert dust, and continental deep-freeze conditions — confirms that CQC Track’s heat-treatment consistency, dimensional precision, anti-corrosion packaging, and logistical reliability meet the universal requirements of the 65–75 tonne excavator class and rotary blast hole drill applications worldwide.
When you specify a CQC Track 141-9655 Drive Sprocket Wheel Assembly for your CATERPILLAR E365 or E374 — or engage us for a custom travel drive component solution — you are installing a component forged within the same OEM ecosystem that supplies the globe’s leading heavy equipment brands. This sprocket represents more than a direct replacement; it embodies a 20-year engineering commitment to maximizing the uptime and productivity of the CATERPILLAR 345/365/374 series and compatible drilling equipment, shift after demanding shift.
This article was authored by Jack of the CQC International Business Team, with sincere appreciation to Philip and Haily for their dedicated support of our global CATERPILLAR undercarriage and travel drive customers.
Products categories
-
Premium Sprocket PC20 PC30 PC40 For Mini Excava...
-

SUMITOMO KRA1665 KRA1109 SH200 CX180 CX210 CX22...
-

Linkbelt 700LX Sprocket Wheel Assembly (KWA0021...
-

Komatsu PC2000-8 / PC2000-11R Mining Excavator ...
-

LIUGONG CLG950/ CLG952 46A0292 Track Sprocket W...
-

SUNWARD SWE500/ SWE600 Drive Sprocket Assembly ...


