
Komatsu Mining Excavator PC850-8R1 / 2AA-27-12120 Sprocket Wheel Assembly – Specialized Manufacturer of Heavy-Duty Crawler Excavator Undercarriage Components for Mining Applications; Supports Non-Standard Customization, Distribution, and Wholesale


The drive sprocket wheel assembly is the torque-transmitting heart of a crawler excavator’s undercarriage. On a mining-class machine like theKomatsu PC850-8R1, the sprocket must convert hydraulic drive power into reliable tractive effort while withstanding continuous abrasive contact, high shock loads, and the relentless demand of production mining. Part number2AA-27-12120is the original sprocket wheel assembly for this platform, and CQCTrack—a specialized manufacturer of heavy-duty crawler excavator undercarriage components—produces it to exacting OEM standards. We support non-standard customization, distribution, and wholesale supply, delivering factory-direct quality to mining operators, equipment dealers, and undercarriage parts distributors worldwide.
1. Manufacturer Strength: Specialized Expertise and OEM Production Credentials
CQCTrack is not a general parts supplier. We are a dedicated undercarriage manufacturer with active OEM production lines currently serving Hitachi, Kobelco, LiuGong, XCMG, and SDLG. This means theKomatsu PC850-8R1sprocket assembly benefits from the same metallurgical controls, casting disciplines, machining tolerances, and heat-treatment protocols that satisfy the rigorous quality standards of Japanese and Chinese heavy equipment leaders. Our engineering team includes specialists who have spent decades focused exclusively on crawler undercarriage design and manufacturing.
Our vertically integrated production infrastructure includes:
- In-house alloy steel casting and forging capabilities for sprocket bodies and hubs.
- CNC turning, boring, hobbing, and profile milling centers for large-diameter sprockets.
- Multi-zone heat-treatment furnaces with computer-controlled quench and temper cycles.
- Medium-frequency induction hardening stations with precision coil design for uniform tooth hardening.
- Coordinate measuring machines (CMM), gear profile testers, and hardness testers for final verification.
- Clean assembly areas for hub, bearing, and seal installation where applicable.
This complete control over the manufacturing chain ensures that every2AA-27-12120sprocket wheel assembly delivers consistent tooth geometry, correct pitch diameter, and predictable wear life—critical factors for maintaining track chain integrity and minimizing downtime in mining operations.
2. Product Description: 2AA-27-12120 Sprocket Wheel Assembly
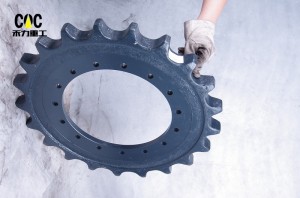
The CQCTrack sprocket wheel assembly for the KomatsuPC850-8R1is engineered as a complete, ready-to-install unit. It is designed to engage the track chain bushings with precision, transferring torque smoothly while protecting both the sprocket and the chain from premature wear.
- Sprocket Body Material: The sprocket rim and body are integrally cast from a specially formulated alloy manganese steel. This material chemistry is selected for its deep hardenability, high toughness, and resistance to sliding-wear fatigue. The casting process produces a near-net shape with a refined grain structure, minimizing internal defects and ensuring consistent hardness response during heat treatment.
- Integral Quenching and Tempering: Following casting, the entire sprocket ring undergoes a full-body quench and high-temperature temper. This through-hardening preliminary treatment homogenizes the microstructure around the full circumference, relieves casting stresses, and creates a uniformly tough, fine-grained matrix from root to tip. This step is essential; a sprocket that is surface-hardened without prior tempering will suffer from a weak subsurface that spalls and deforms under the crushing roller path of a mining excavator.
- Precision Machining: The stabilized, tempered ring is then set up on heavy-duty CNC machining centers. The central mounting bore, bolt hole pattern, pilot diameter, and every sprocket tooth flank are machined to exact profile. By performing all precision material removal after the initial through-tempering, CQCTrack eliminates dimensional drift that would otherwise be locked in during final heat treatment. The result is a sprocket that mounts to the final drive hub with zero runout and engages the track chain bushings with full-face contact from the first revolution.
- Final Overall Induction Hardening: The fully machined sprocket assembly then enters the medium-frequency induction hardening station. Here, the entire tooth profile—including the working flanks, root radii, and tip surfaces—is rapidly and uniformly austenitized and quenched in a controlled process. This produces a deep, continuous hardened case precisely where wear and contact stress occur, while the previously tempered core remains ductile and impact resistant. The surface hardness is stringently maintained within the range of 52 to 58 HRC. This hardness window is a deliberate engineering choice. It is high enough to dramatically resist abrasive grooving caused by compacted mine fines and the rolling-contact fatigue that pits tooth flanks, yet it is correctly balanced to be marginally softer than the fully carburized track chain bushings. This critical hardness differential ensures that normal wear is sacrificially absorbed by the sprocket rather than the far more labor-intensive track chain, preserving bushing life and maintaining perfect chain pitch without inflicting premature damage to the track links.
- Perfect Chain Harmony: The combination of precise cast tooth geometry, full induction hardened profile, and optimal hardness matching means the CQCTrack 2AA-27-12120 sprocket achieves a low-friction, low-noise mesh with the Komatsu track chain. It will not climb, skip, or gouge the bushings, extending the service life of the complete undercarriage system.
3. Non-Standard Customization, Distribution, and Wholesale Support
As a specialized manufacturer, CQCTrack offers more than standard replacement parts. We provide:
- Non-Standard Customization: We can adapt sprocket dimensions, tooth counts, hardness profiles, and material specifications to meet specific customer requirements, alternative part numbers, or unique mining applications. Our engineering team works directly with clients to develop tailored solutions.
- Distribution Support: We supply undercarriage parts distributors with reliable, factory-direct inventory and technical documentation.
- Wholesale Supply: We offer competitive pricing for bulk orders, container-load quantities, and long-term supply agreements.
4. Twenty Years of Process Evolution and Global Field Validation
The CQCTrack Komatsu PC850-8R1 sprocket wheel assembly is the product of more than 20 years of continuous undercarriage manufacturing experience. Our process technology has been expanded and refined through a closed-loop feedback system that captures field performance data from every major market we serve. Adjustments to alloy chemistry, casting parameters, machining sequences, induction hardening parameters, and tooth profile design have been permanently incorporated into our production standards.
This sprocket has been repeatedly validated in the world’s most severe operating environments:
- The abrasive, silica-rich copper and gold mines of South America, including Ecuador and Peru.
- The hard-rock and high-impact mining sites of South Africa.
- The frozen, ice-bound overburden of Russia and Kazakhstan.
- The high-humidity, corrosive conditions of South Pacific island mining projects.
- The demanding mixed terrain of South Korea, India, Vietnam, North America, and Turkey.
In each environment, the CQCTrack sprocket wheel assembly has demonstrated stable tooth wear, reliable torque transmission, and structural integrity. Mining fleet managers can plan undercarriage maintenance with confidence rather than reacting to unexpected sprocket failure.
5. Related Undercarriage Components and System Compatibility
CQCTrack manufactures the Komatsu PC850-8R1 sprocket wheel assembly as part of a complete crawler undercarriage system. We also produce the matching components for this excavator platform:
- Track lower roller assemblies./209-30-00191SF /209-30-00310DF
- Front idler wheel assemblies./209-30-00014
- Top carrier roller groups./209-30-00300
- Track chains with heat-treated pins and bushings.
- Track shoesAssembly./209-32-02000;209-32-02050
By sourcing all rolling and drive wear components from a single, OEM-aligned manufacturer, mining operations ensure full metallurgical and dimensional compatibility across the entire undercarriage. This eliminates the accelerated wear caused by mixing parts from disconnected suppliers.
6. Direct Global Export and Distribution Network
CQCTrack exports the Komatsu PC850-8R1 sprocket wheel assembly and related undercarriage components directly from our factory to customers across the globe. Our regular export destinations include:
- South America: Ecuador, Peru, and other Andean mining markets.
- Africa: South Africa and neighboring hard-rock mining regions.
- Russia and Central Asia: Russia, Kazakhstan, and CIS countries.
- Premium Asia-Pacific Markets: South Korea, India (high-end product segments), Vietnam, and South Pacific island nations.
- North America and EMEA: North America and Turkey.
Our international business team manages export documentation, container loading, and urgent spare-parts logistics to ensure that mining operations receive the right sprocket assembly at the right time.
CQC International Business Team: Philip | Jack | Haily
This product introduction has been personally authored and technically reviewed by Jack from the CQCTrack Global Business Division, based on current manufacturing specifications and verified field performance data for the Komatsu PC850-8R1 sprocket wheel assembly, part number 2AA-27-12120.
Products categories
-
Excavator sprocket PC100 PC120 203-27-51310 203...
-

LIUGONG 46A0185 CLG970 CLG975 Track Sprocket Wh...
-

Komatsu 2092751172 2092751173 2092751170 PC800 ...
-

Engineering the SANY SY870H Drive Sprocket Asse...
-

Caterpillar 8E9805 CR5602 CR6998 ZZYS0031 E318 ...
-

SUNWARD SWDM360 Rotary Drilling Rig Chassis Com...


